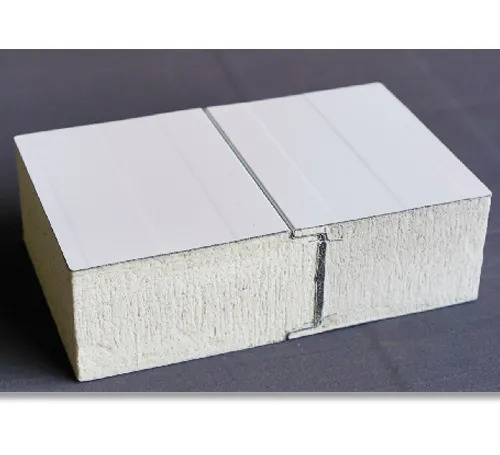
Headstream Cold Store Panels: Engineered Excellence for Reliable Cold Chain Infrastructure

In today’s fast-growing global cold chain industry, maintaining precise temperature control while minimizing energy consumption and ensuring food safety has become more critical than ever. Headstream Panel(https://www.headstreampanel.com/), a trusted name in high-performance building materials, offers specialized Cold Store Panels(https://www.headstreampanel.com/products/cold-store-panels/) that deliver outstanding thermal efficiency, structural integrity, and operational reliability for modern cold storage facilities. As demand surges for refrigerated warehouses, processing plants, and logistics hubs, these panels provide a complete system solution—including walls, roofs, floors, doors, and supporting structures—designed specifically to meet the stringent requirements of temperature-sensitive environments.

Unlike general insulated panels that serve broad construction needs, Headstream’s Cold Store Panels are purpose-built for low-temperature applications. They form airtight, high-insulation envelopes capable of sustaining temperatures from ambient down to -40°C or lower, making them indispensable for food preservation, pharmaceutical storage, frozen logistics, and agricultural produce facilities. By integrating advanced core materials with robust cam-lock connection systems, these panels help operators achieve lower energy bills, faster installation, and long-term durability even under harsh operating conditions.

Why Cold Storage Demands Specialized Panel Systems

Traditional construction methods using brick, concrete, or standard sandwich panels often fall short in cold room environments. Issues such as thermal bridging, moisture ingress, ice formation, and poor airtightness can lead to higher refrigeration loads, condensation problems, and potential contamination risks. Headstream Cold Store Panels address these challenges directly through optimized design and material selection.

The panels typically feature high-density polyurethane or enhanced PIR cores known for their low thermal conductivity, which dramatically reduces heat transfer. This results in superior energy efficiency—allowing refrigeration systems to work less while maintaining stable internal temperatures. The cam-lock (eccentric hook) connection system creates strong, seamless joints that enhance airtightness and structural stability, preventing cold air leakage and minimizing the risk of ice buildup at panel interfaces.

Additional system components include:

  • Insulated wall and roof panels with consistent thickness options to match specific temperature requirements.
  • Floor panels engineered for heavy load-bearing while retaining excellent insulation properties.
  • Specialized cold room doors with matching insulation performance and sealing technology.
  • Supporting plates and base structures that ensure level installation and long-term stability.

This integrated approach transforms cold storage construction from a complex, time-consuming process into a modular, efficient assembly that can be completed significantly faster than conventional methods.

Technical Advantages Driving Performance

Headstream emphasizes FM Approval for many of its cold storage solutions, underscoring a commitment to internationally recognized safety and performance standards. Key technical strengths include:

  • Exceptional Thermal Performance: The core materials are selected and formulated to deliver minimal heat gain, helping facilities maintain ultra-low temperatures with reduced compressor runtime and lower electricity costs.
  • High Airtightness and Moisture Resistance: Precision-engineered joints and surface treatments prevent humid air infiltration, reducing the formation of frost and extending the lifespan of both the panels and the refrigeration equipment.
  • Structural Strength and Load Capacity: Panels are designed to withstand internal pressure differences, external wind loads, and heavy racking systems common in modern warehouses, ensuring safety and operational flexibility.
  • Fire Safety Considerations: While thermal insulation is the priority, the panels incorporate materials that contribute to overall fire performance, an important factor in large-scale cold storage facilities handling flammable goods or operating in high-risk areas.
  • Hygiene and Easy Maintenance: Smooth, cleanable surfaces and corrosion-resistant finishes support strict sanitation protocols required in food and pharmaceutical cold chains.

Customization is another standout feature. Headstream works closely with clients to tailor panel thickness, dimensions, core density, and surface coatings according to the target storage temperature, facility size, and regional climate conditions. Whether for a small blast freezer or a massive multi-compartment distribution center, the panels can be adapted to deliver optimal results.

Real-World Applications Across the Cold Chain

Headstream Cold Store Panels serve a wide spectrum of industries where temperature control is non-negotiable:

  • Food Industry: From fresh produce and dairy to meat, seafood, and frozen ready meals, these panels help maintain the cold chain from processing to distribution, preserving quality and extending shelf life.
  • Pharmaceutical and Biotechnology: Strict temperature stability is essential for vaccines, biologics, and sensitive medicines. The panels’ reliable insulation and airtight performance support GMP-compliant environments.
  • Cold Chain Logistics: Modern refrigerated warehouses and cross-docking facilities benefit from quick assembly and energy-efficient design, enabling faster turnaround times and lower operating expenses.
  • Agriculture and Seafood: Controlled-atmosphere storage for fruits, vegetables, and fresh catches relies on the panels’ ability to create stable, low-humidity conditions.
  • Chemical and Industrial Storage: Certain temperature-sensitive raw materials and finished goods also require specialized cold environments.

In each case, the panels contribute not only to product integrity but also to sustainability goals by reducing energy consumption and associated carbon emissions.

Complementary Products Enhancing Cold Storage Solutions

While Cold Store Panels form the heart of temperature-controlled facilities, Headstream offers a broader portfolio that integrates seamlessly to create comprehensive building envelope systems.

Insulated Panels(https://www.headstreampanel.com/products/insulated-panel/) provide versatile options for non-critical areas within or adjacent to cold storage complexes, such as ante-rooms, office sections, or loading bays. Their polyurethane, rock wool, or glass wool cores deliver reliable thermal and weather resistance, allowing architects to maintain design consistency across the entire project while optimizing costs.

For facilities requiring the highest levels of hygiene—such as ready-to-eat food processing zones or pharmaceutical clean production areas—Clean Room Panels (https://www.headstreampanel.com/products/clean-room-panels/)deliver superior airtightness, easy-to-clean surfaces, and contamination control. These panels complement cold store solutions by ensuring that adjacent processing or packaging areas meet stringent cleanliness standards without compromising thermal performance.

In budget-sensitive projects or for secondary structures like staff facilities and general warehouses, EPS Sandwich Panels(https://www.headstreampanel.com/products/eps-sandwich-panel/) offer a lightweight, cost-effective alternative with good thermal insulation and rapid installation. Their clean aesthetic and solid performance make them suitable for supporting infrastructure around main cold storage units.

This full-range capability allows developers and contractors to source all necessary sandwich panel solutions from a single reliable partner, simplifying procurement, ensuring material compatibility, and streamlining project timelines.

Sustainable Benefits and Future Outlook

Beyond immediate performance, Headstream Cold Store Panels support broader sustainability objectives. Their high insulation values directly lower the energy demand of refrigeration systems, which often account for the largest portion of a cold storage facility’s electricity use. Reduced energy consumption translates into lower operational costs and a smaller carbon footprint—critical advantages as regulations tighten and companies pursue net-zero targets.

The modular nature of the panels also promotes faster construction with less on-site waste compared to traditional methods. Many components are designed for potential disassembly and reuse, aligning with circular economy principles in the building sector.

Looking forward, the cold chain industry continues to expand rapidly, driven by e-commerce growth, global food trade, and the need for secure pharmaceutical distribution. Headstream remains focused on continuous innovation—exploring even lower-conductivity core materials, smarter integration with monitoring systems, and enhanced fire-resistant formulations to meet evolving market demands.

Choosing Headstream for Your Next Cold Storage Project

When selecting materials for cold storage, decision-makers prioritize proven reliability, technical support, and total cost of ownership. Headstream stands out through its combination of advanced manufacturing, international certifications, and a customer-centric approach that includes technical consultation and after-sales service.

Projects benefit from:

  • Reduced construction time through modular cam-lock assembly.
  • Lower lifetime energy costs thanks to superior insulation.
  • Enhanced safety and compliance with industry standards.
  • Flexible design options that adapt to specific operational needs.

Whether you are planning a new state-of-the-art distribution center, expanding an existing facility, or upgrading older cold rooms, Headstream Cold Store Panels deliver a future-ready solution that balances performance, efficiency, and value.

To learn more about tailored cold storage panel systems or to discuss your project requirements, visit the official website(https://www.headstreampanel.com/).
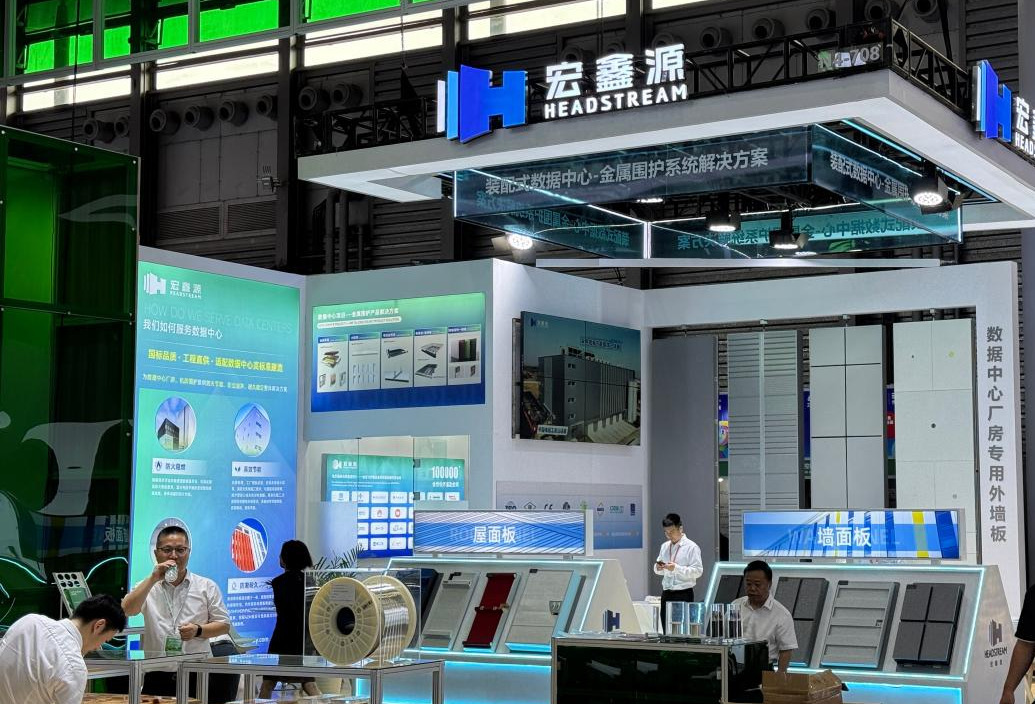
Grand Success | HEADSTREAM Showcases Full-Scenario Data Center Building Envelope Solutions at IDCE 2026

On June 3, at the globally renowned 2026 International Data Center Industry Exhibition (IDCE), HEADSTREAM made another remarkable appearance, presenting its innovative green building materials and full-scenario data center building envelope solutions. The booth attracted a large number of professional visitors and industry experts for in-depth discussions.


01 | Exhibition Highlights

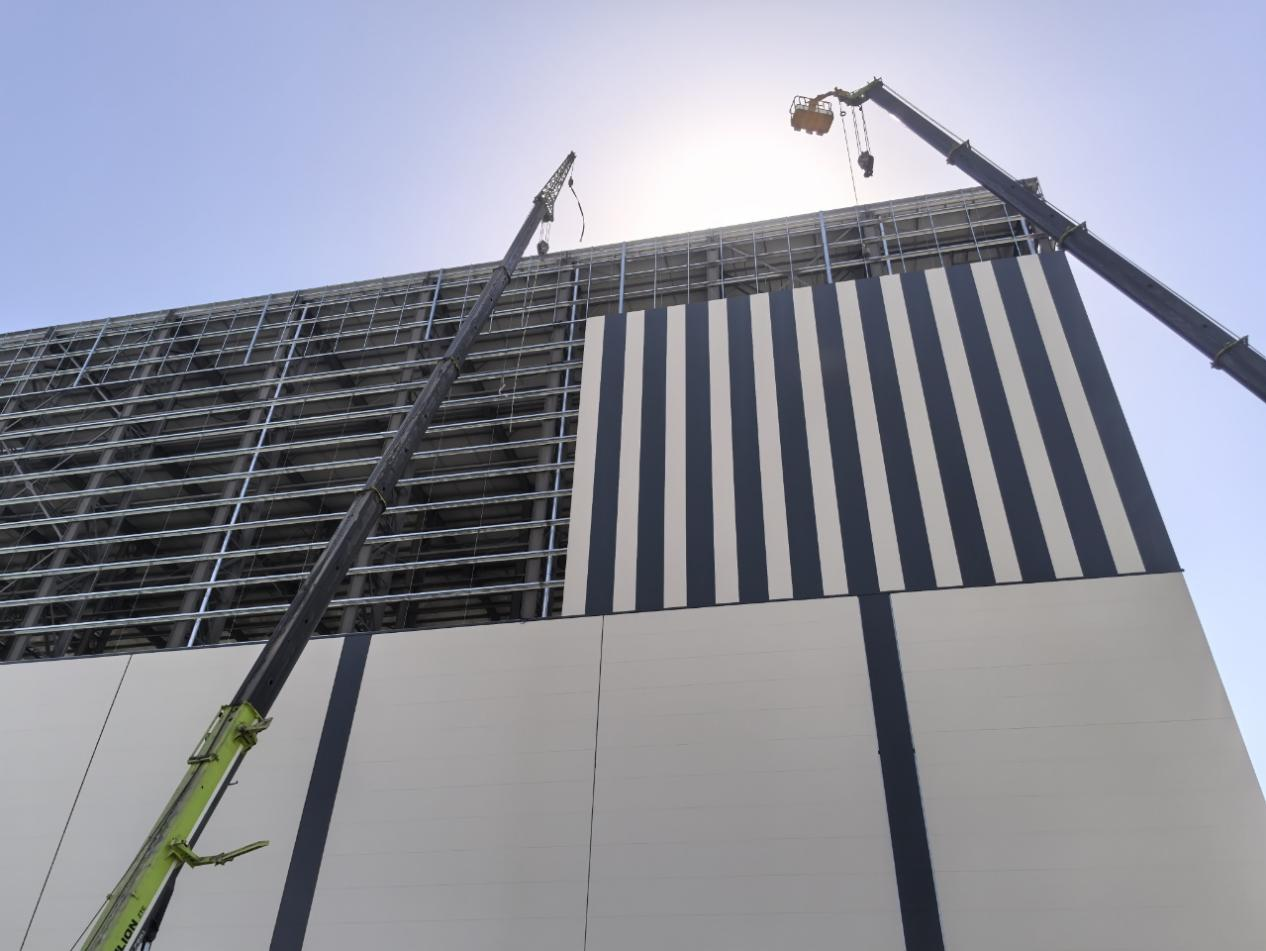
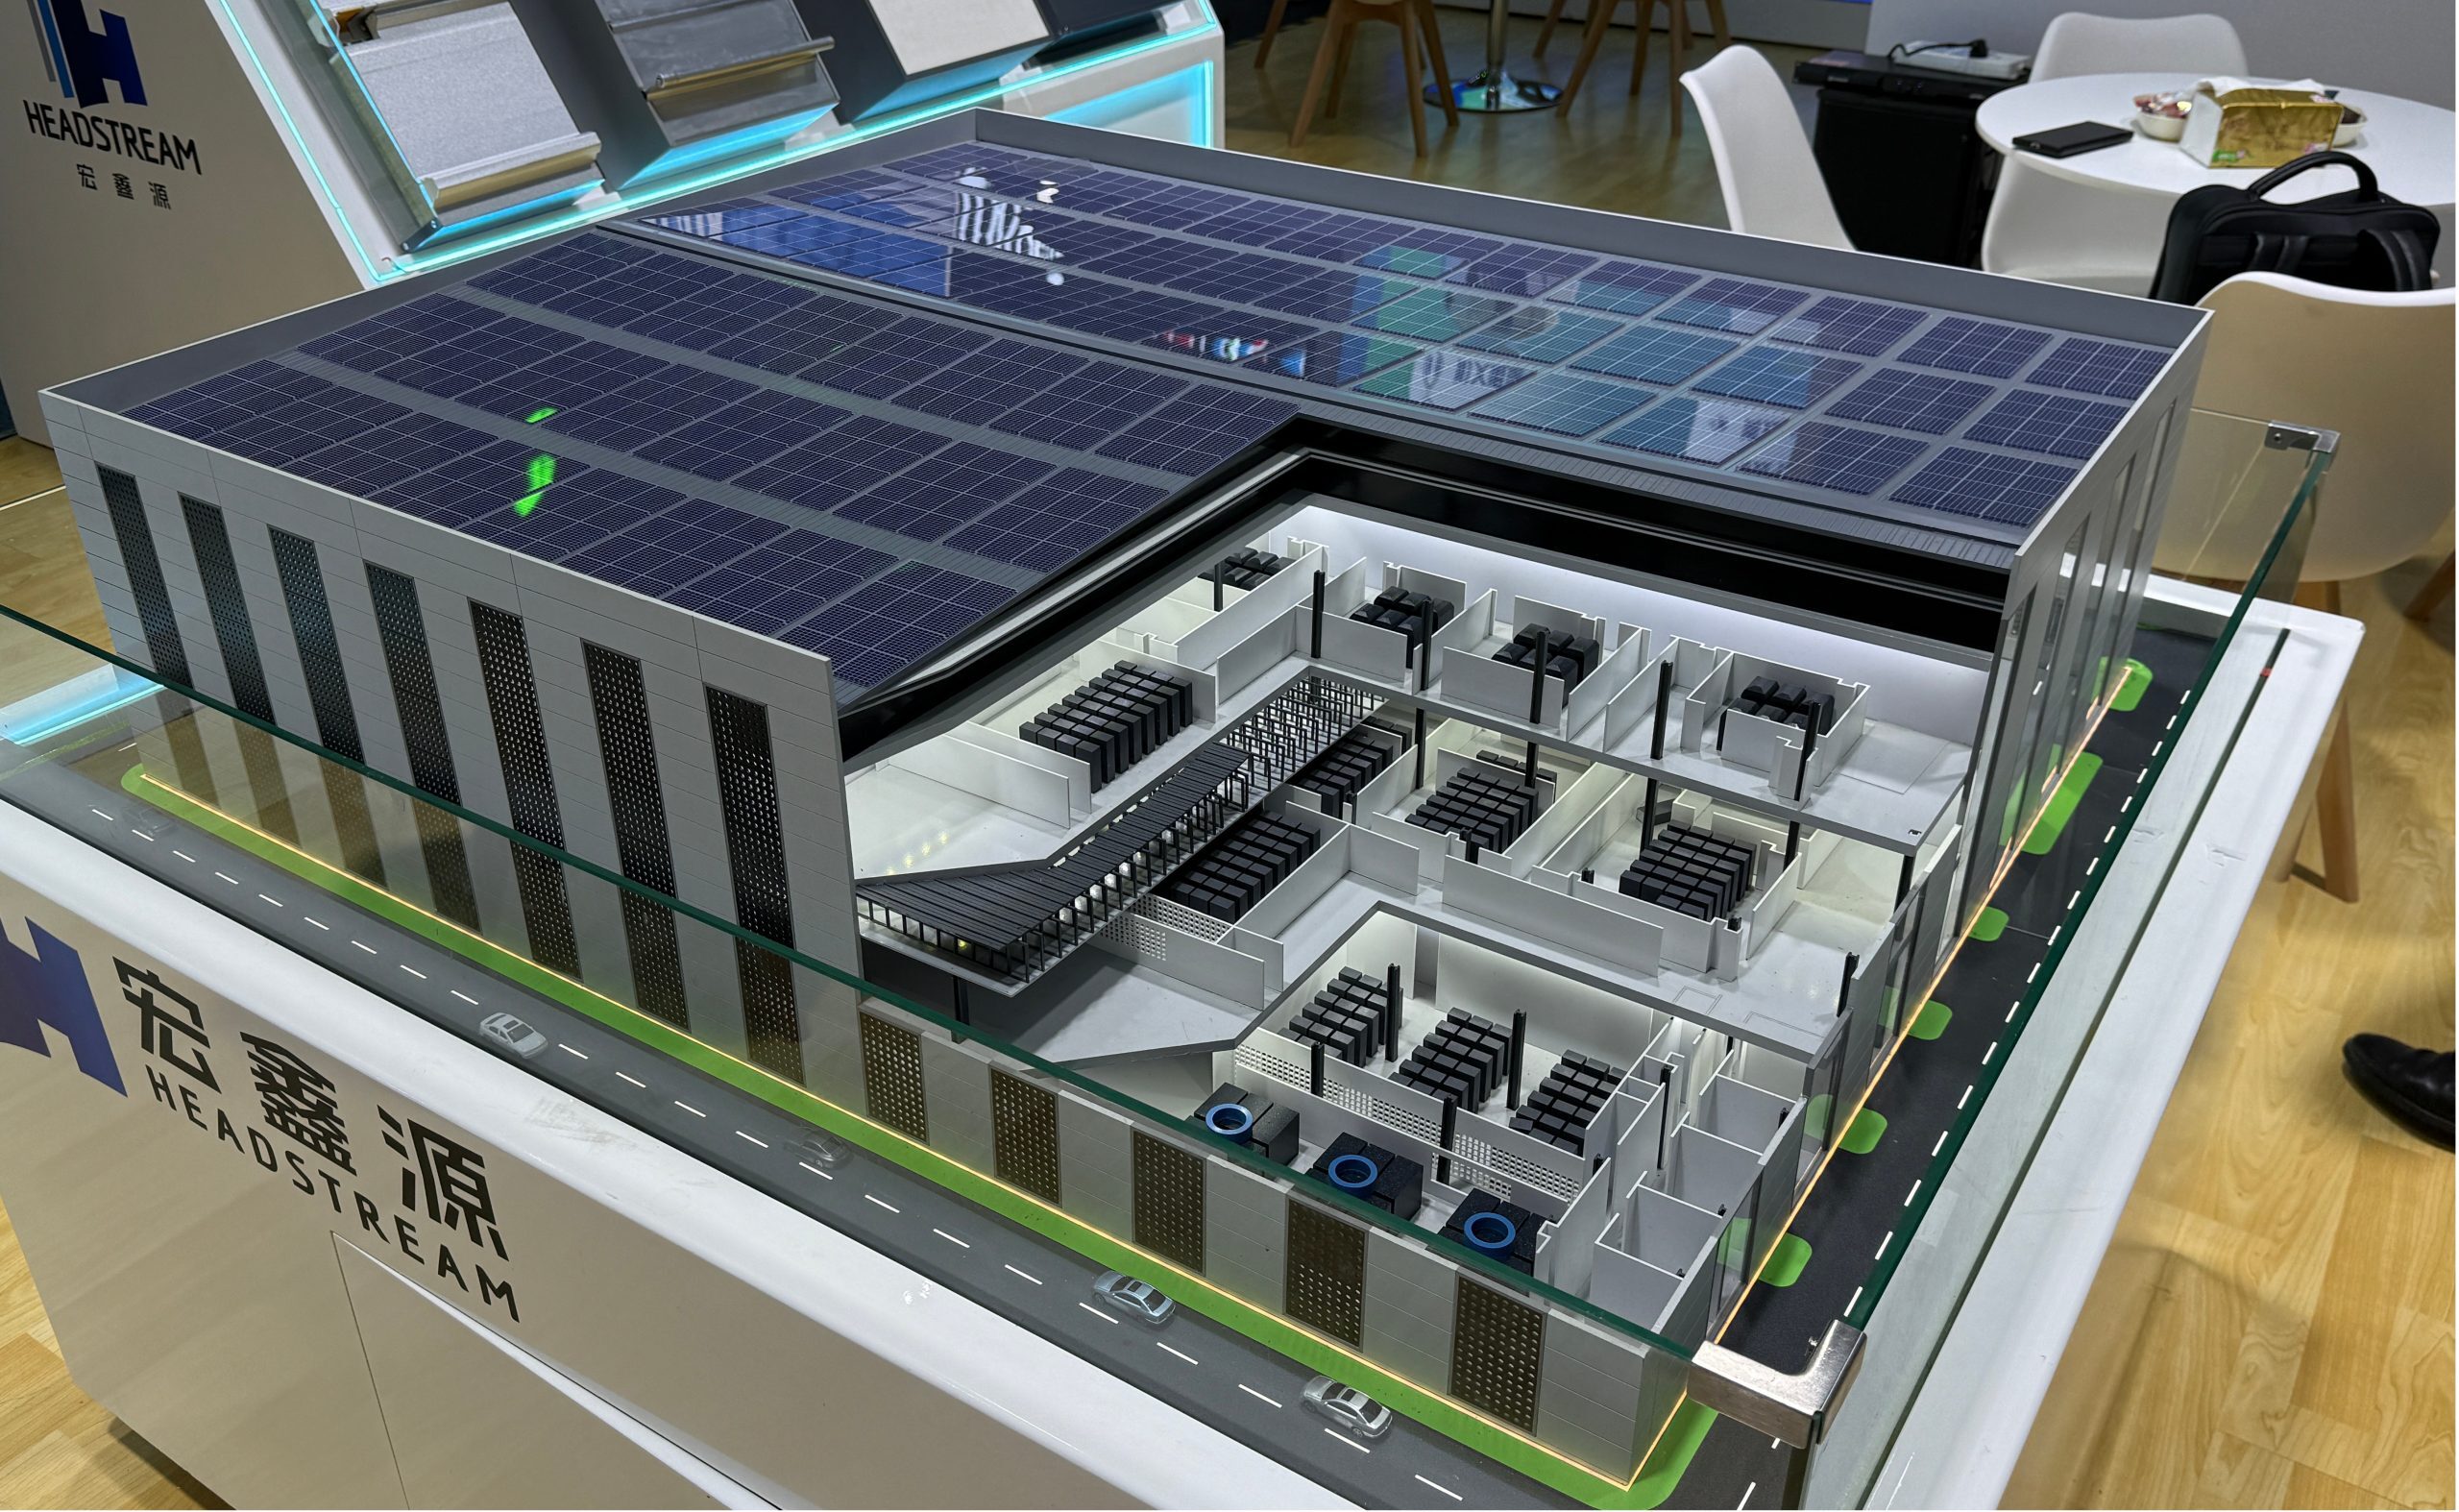
At the exhibition site, HEADSTREAM showcased a real-life model of its data center building envelope system, which drew significant attention from data center operators, design institutes, and industry representatives.

The interactive display provided new insights into intelligent construction for data centers, offering advanced approaches to building safety, energy efficiency improvement, and operational optimization.

HEADSTREAM’s technical team engaged in in-depth discussions with visitors on key topics such as:

  • Data center structural safety and protection systems
  • Energy efficiency enhancement strategies
  • Operation and maintenance optimization solutions

02 | Full-Scenario Coverage of Data Center Envelope Systems

To meet the diverse functional requirements of modern data centers, HEADSTREAM presented a wide range of building envelope system solutions tailored for different application scenarios.

The solutions demonstrate outstanding performance in:

  • Structural safety compliance
  • Energy conservation and efficiency improvement
  • Fire resistance and explosion relief performance

Whether for hyperscale data centers with extremely high safety standards, cloud computing facilities requiring strict environmental stability, or energy storage supporting infrastructure, HEADSTREAM provides fully customized and system-integrated envelope solutions.

03 | System Innovation Driving Project Implementation

From core materials to integrated building envelope systems, HEADSTREAM applies a system-level engineering approach to deliver a complete product ecosystem for the data center industry.

This end-to-end solution portfolio fully meets the increasingly diversified and refined demands of modern infrastructure development.

With strong technological expertise, HEADSTREAM’s integrated solutions have already been applied in multiple advanced sectors, including:

  • Hyperscale data centers
  • New energy storage industrial parks
  • Semiconductor cleanroom facilities

These solutions provide long-term, stable, and reliable protection for landmark projects worldwide.

Building a Zero-Carbon Digital Future

Looking ahead, HEADSTREAM will continue to drive innovation through advanced material systems, focusing on developing safer, more efficient, and more sustainable building envelope solutions.

By empowering the global data center industry, HEADSTREAM is committed to accelerating the transition toward a zero-carbon and intelligent digital era, delivering high-performance infrastructure solutions for the future.

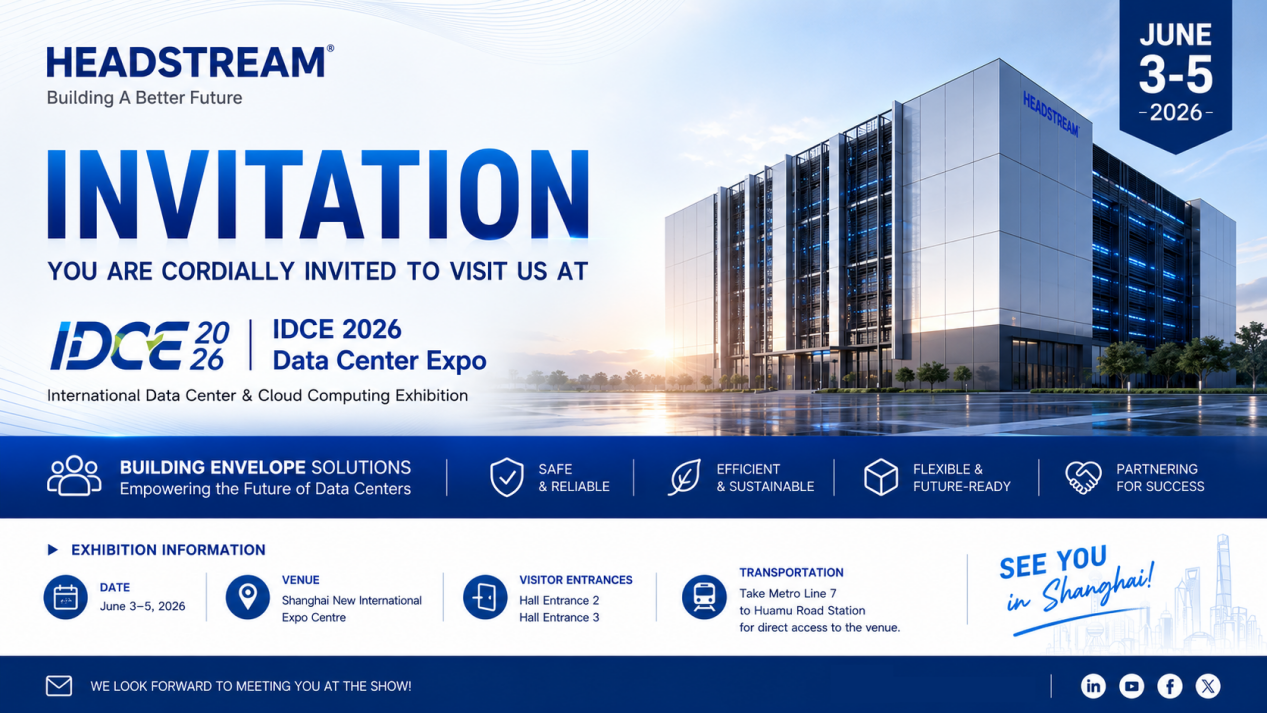
Exhibition Invitation | Meet HEADSTREAM at IDCE 2026 Data Center Expo, June 3–5

As AI technologies and the computing economy continue to accelerate, data center construction is entering a new era of higher density, enhanced security, and greater operational efficiency.

From June 3–5, HEADSTREAM will participate in the 2026 IDCE Data Center Expo at the Shanghai New International Expo Center, showcasing advanced metal building envelope solutions designed specifically for modern data centers.

We sincerely invite global partners, contractors, developers, and industry professionals to visit our booth and explore the future of high-performance data center construction together.

HEADSTREAM Metal Building Envelope Systems

Full-Scenario Solutions for Modern Data Centers

HEADSTREAM provides integrated building envelope systems that help improve safety, energy efficiency, operational stability, and long-term scalability for data center projects.

Fire Protection & Safety

Our systems utilize Class A fire-resistant materials combined with advanced joint sealing technology to effectively slow flame spread and reduce smoke diffusion risks, ensuring enhanced protection for critical equipment and personnel.

Waterproof & Leak Prevention

The Level-1 waterproof roofing system and concealed fastening design help eliminate leakage risks in roofs and wall systems, minimizing the possibility of equipment damage and data loss.

Explosion Venting & Structural Protection

HEADSTREAM explosion venting wall panels are engineered to release shock waves in a controlled direction, helping protect the integrity of the main structure. At the same time, the system maintains excellent thermal insulation, wind resistance, and structural safety performance for high-risk areas.

Green Energy Integration

Our Building-Integrated Photovoltaic (BIPV) solutions transform roofs and façades into energy-producing assets, supporting stable and sustainable power supply systems for data centers.

Flexible & Future-Ready Design

With modular construction and long-span structural systems, HEADSTREAM solutions allow reserved space for pipelines, equipment upgrades, and future expansion without large-scale demolition, helping data centers adapt easily to evolving technologies.

Why Choose HEADSTREAM for Data Centers?

HEADSTREAM metal building envelope systems help data centers achieve:

Faster project construction

Stable long-term operation

Improved energy efficiency

Reduced maintenance costs

Flexible future expansion

Visitor Information

Exhibition

IDCE 2026 Data Center Expo

Date

June 3–5, 2026

Venue

Shanghai New International Expo Centre

Visitor Entrances

Hall Entrance 2 & Hall Entrance 3

Transportation

Take Metro Line 7 to Huamu Road Station for direct access to the venue.

We look forward to meeting you at IDCE 2026 and discussing the future of intelligent, sustainable, and high-performance data center infrastructure with HEADSTREAM.


Energy-Efficient Cold Room Panels for Modern Refrigeration Projects

Energy efficiency has become a top priority in the refrigeration and cold chain industry. High-performance cold room panels are now widely used to create reliable and sustainable temperature-controlled environments for industrial and commercial applications.

Modern insulated panels are engineered to reduce heat transfer, improve temperature stability, and lower operating costs. With rising global energy prices, efficient cold room construction materials are becoming increasingly valuable for businesses worldwide.

Advanced Insulation Technology

Cold room panels typically use advanced insulation cores such as PIR or PU foam. These materials provide:

  • Low thermal conductivity
  • Excellent airtightness
  • Reduced energy loss
  • Improved temperature retention

Compared with traditional construction materials, insulated sandwich panels significantly improve refrigeration efficiency.

Durable Structure for Long-Term Use

Cold storage environments are demanding. Panels must withstand:

  • Moisture exposure
  • Low temperatures
  • Frequent cleaning
  • Heavy daily operation

High-quality cold room panels are manufactured with durable steel surfaces and corrosion-resistant coatings to ensure long service life.

Fast Installation and Flexible Design

Modern panel systems feature modular designs that allow for:

  • Quick installation
  • Flexible room sizing
  • Easy expansion
  • Reduced labor costs

This makes them ideal for projects with tight construction schedules.

Common Cold Room Applications

Energy-efficient insulated panels are widely used in:

  • Meat and seafood storage
  • Fruit and vegetable preservation
  • Dairy product refrigeration
  • Medical and pharmaceutical storage
  • Logistics and distribution centers

Different temperature requirements can be achieved by selecting suitable panel thicknesses and refrigeration systems.

Sustainable Cold Storage Solutions

Energy-saving cold room panels help businesses reduce carbon emissions while lowering operational expenses. As sustainability regulations become stricter worldwide, insulated cold storage systems are increasingly important for environmentally responsible construction.

Conclusion

Modern cold room panels provide an ideal combination of thermal insulation, durability, and installation efficiency. For businesses investing in refrigeration infrastructure, high-quality insulated panels offer long-term energy savings and reliable cold storage performance.

Cleanroom Panels for Pharmaceutical and Food Industry Applications

As hygiene standards continue to rise across the pharmaceutical, electronics, food processing, and healthcare industries, cleanroom panels have become an essential building material for controlled environments. Modern cleanroom systems require wall and ceiling solutions that provide excellent airtightness, easy cleaning, fire resistance, and long-term durability.

Cleanroom panels are specifically designed to meet strict environmental requirements while improving operational efficiency and maintaining high cleanliness standards.

What Are Cleanroom Panels?

Cleanroom panels are insulated sandwich panels used in controlled environments where dust, bacteria, humidity, and temperature must be carefully managed. These panels are widely used in cleanrooms, laboratories, operating rooms, and precision manufacturing facilities.

Typical cleanroom panel structures include:

  • Color-coated steel surfaces
  • Insulation core materials
  • Sealed connection systems
  • Smooth and hygienic finishes

Common insulation cores include rock wool, PIR, PU, and glass magnesium materials.

Core Advantages of Cleanroom Panels

Excellent Hygienic Performance

Cleanroom panels feature smooth surfaces that are easy to clean and resistant to dust accumulation. This helps maintain sterile environments in industries with strict hygiene standards.

Fire Resistance

Many cleanroom projects require fire-resistant materials. High-quality cleanroom panels can achieve strong fire protection performance while maintaining structural stability.

Thermal and Acoustic Insulation

Insulated cleanroom panels help control indoor temperature and reduce noise transmission, improving working conditions and energy efficiency.

Fast Installation

Modular cleanroom panel systems allow rapid installation and flexible room partitioning, reducing project construction time.

Typical Applications

Cleanroom panels are widely used in:

  • Pharmaceutical factories
  • Food processing workshops
  • Electronics manufacturing plants
  • Hospitals and operating rooms
  • Biotechnology laboratories
  • Cosmetic production facilities

Different industries may require different cleanroom classifications and panel specifications.

Choosing the Right Cleanroom Panel Supplier

When selecting cleanroom panels, buyers should focus on:

  • Fire resistance rating
  • Surface coating quality
  • Airtight connection systems
  • Corrosion resistance
  • Installation support
  • Industry certification

Professional manufacturers can provide customized cleanroom solutions based on project requirements.

Conclusion

Cleanroom panels play a critical role in creating safe, hygienic, and controlled environments for modern industrial applications. With excellent insulation, fire resistance, and easy maintenance, cleanroom panel systems have become an ideal solution for pharmaceutical, food, medical, and electronics industries worldwide.

Can Rock Wool Panels Improve Fire Safety in Buildings?

Introduction
Fire safety is a critical concern in modern construction, especially for industrial and commercial buildings. Rock wool sandwich panels are often recommended for their fire-resistant properties—but how effective are they?

Fire Resistance Performance
Rock wool is a non-combustible material with a high melting point. Panels made with rock wool cores can achieve top fire ratings (such as A1 classification), meaning they do not contribute to fire spread.

Thermal Stability
Unlike some insulation materials, rock wool maintains its structure even under high temperatures. This helps contain fires and provides more time for evacuation and firefighting.

Safety Benefits
Using rock wool panels can significantly reduce fire risks, protect structural integrity, and enhance overall building safety.

Applications

  • Industrial plants
  • Power stations
  • Warehouses storing flammable goods

Conclusion
Rock wool panels are an excellent choice for improving fire safety. Their non-combustible nature and thermal stability make them ideal for high-risk environments.

CTA
Enhance your building’s fire protection with HEADSTREAM rock wool panels. Contact us today for expert guidance.

Building a Clean Room: Key Requirements and Why Headstream Clean Room Panels Excel

Constructing an effective clean room is a precise engineering task that requires strict control over airborne particles, temperature, humidity, pressure differentials, and overall environmental stability. Industries such as pharmaceuticals, biotechnology, electronics manufacturing, semiconductor production, medical devices, and food processing all depend on these controlled spaces to safeguard sensitive products and maintain high production standards.

Core requirements for building a successful clean room typically include:

  • Effective Particle and Contamination Control: Advanced air filtration combined with carefully managed pressure cascades to prevent unwanted particles or microbes from entering critical zones.
  • Superior Airtight Construction: The entire building envelope—walls, ceilings, and floors—must form a highly sealed barrier with minimal air leakage to sustain required pressure differences and block external contaminants.
  • Smooth, Non-Shedding Surfaces: Interior surfaces need to be durable, impervious to moisture, resistant to frequent cleaning with disinfectants, and designed to generate as few particles as possible over time.
  • Excellent Thermal and Humidity Stability: High-performance insulation is essential to reduce energy use in HVAC systems that run continuously to maintain precise temperature and moisture levels.
  • Fire Resistance and Structural Integrity: Materials must offer reliable fire performance while withstanding mechanical stresses and repeated cleaning cycles without degrading.
  • Modular Flexibility: The system should allow quick installation, easy reconfiguration, and minimal disruption during setup or future modifications.
  • Long-Term Reliability and Maintainability: Surfaces and joints must remain cleanable and stable for years, supporting consistent operation with lower maintenance demands.

Traditional building approaches using concrete, masonry, or standard wall systems often introduce challenges such as dust generation during construction, thermal bridging that increases energy costs, potential cracking that can trap contaminants, and extended installation timelines. These limitations make specialized Clean Room Panels(https://www.headstreampanel.com/products/clean-room-panels/) the modern, preferred choice for creating high-performance controlled environments efficiently and reliably.

Headstream Panel, a prominent manufacturer with six state-of-the-art production bases in Shandong, Anhui, Hubei, Chongqing, Guangxi, and Guangdong provinces in China, has developed a dedicated line of Clean Room Panels tailored for these demanding applications. With eight overseas branches in Malaysia, Thailand, Vietnam, the Philippines, Indonesia, Egypt, Algeria, and the United Arab Emirates, the company serves customers across more than 100 countries. Headstream combines advanced manufacturing technology with rigorous quality control and international certifications including FM, CIDB, and ISO to deliver consistent, high-quality solutions.


Headstream Clean Room Panels: Precision-Engineered for Controlled Environments

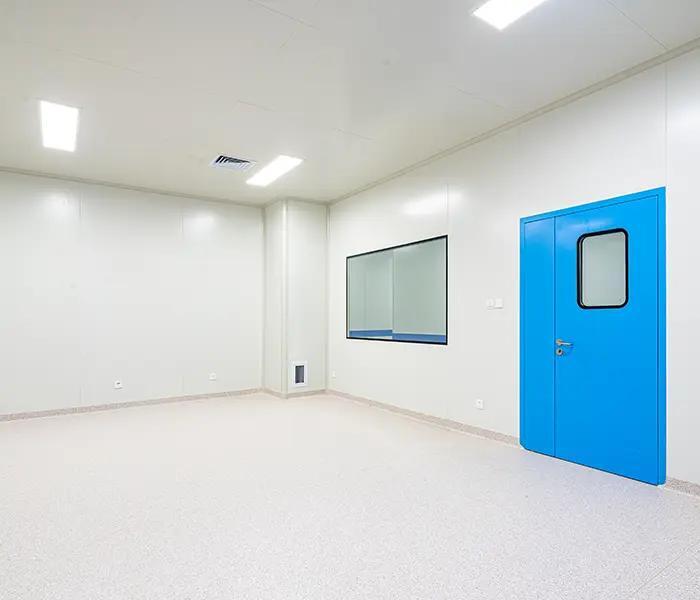
Headstream Clean Room Panels are sandwich-type wall and ceiling systems specifically designed to meet the rigorous demands of contamination-sensitive spaces. They feature high-performance core materials paired with smooth, cleanable surface finishes to create seamless, airtight barriers.

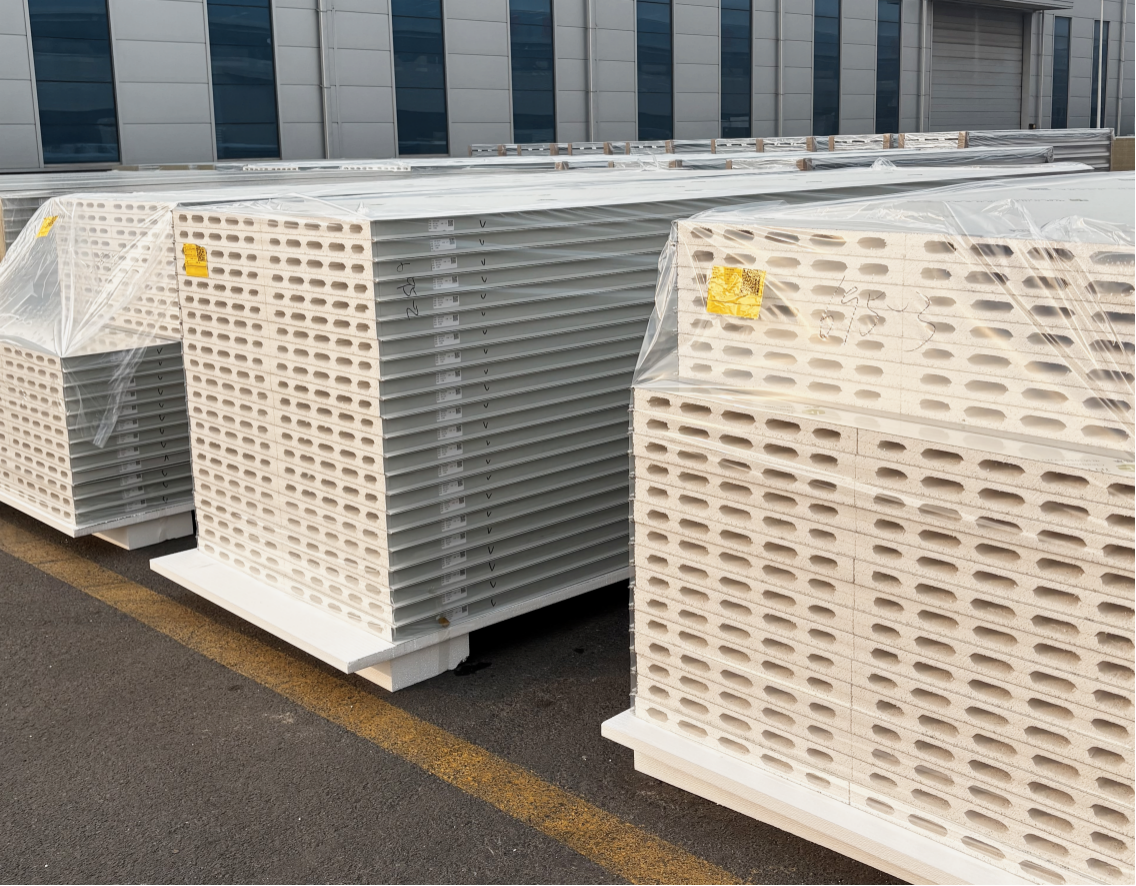
Available core options include polyurethane (PU) for outstanding thermal insulation and lightweight strength, as well as rock wool for superior fire resistance. These cores provide excellent thermal efficiency, helping HVAC systems maintain stable conditions while significantly lowering energy consumption—an important consideration for facilities where climate control systems operate around the clock.

The panels achieve superior airtightness through precision-engineered connection systems that minimize gaps and leakage points. This supports reliable pressure differentials and reduces the risk of external contaminants entering the controlled area. Surface treatments are selected for durability and resistance to common cleaning agents, ensuring surfaces remain smooth and non-shedding even after years of intensive use.

Notable advantages of Headstream Clean Room Panels include:

  • Exceptional Airtight Performance: Tight joints reduce air leakage, enhancing contamination control and improving overall energy efficiency.
  • Strong Thermal Insulation: Low heat transfer rates decrease the workload on air handling units and support stable environmental conditions.
  • Easy Cleaning and Long-Term Durability: Smooth, robust surfaces withstand frequent sanitation without cracking, delaminating, or generating particles.
  • Customization Options: Panels can be tailored in terms of core type, thickness, dimensions, and finishes to match specific cleanliness classes, temperature needs, and project requirements.
  • Rapid Modular Installation: The system allows faster assembly compared to traditional methods, shortening project timelines and reducing on-site contamination risks during construction.

These features make the panels highly suitable for electronics assembly areas, semiconductor fabrication zones, biotechnology research facilities, medical device production spaces, and food processing environments where strict environmental control is essential.

From Clean Room Requirements to Practical Implementation

When designing a clean room, the building envelope plays a foundational role in achieving and maintaining the desired performance. Headstream panels(https://www.headstreampanel.com/) integrate smoothly into modular layouts, enabling flush joints, integrated utility penetrations, and coved transitions with minimal field modifications. Their quick installation process helps project teams complete facilities faster while limiting dust and disruption during the build phase.

In electronics and semiconductor manufacturing, the panels’ low particle generation and stable thermal properties help protect delicate components and processes. In biotechnology and medical device production, their reliable airtightness and cleanable surfaces support consistent environmental conditions. Food processing facilities benefit from the moisture resistance and durability that help maintain hygiene standards throughout production zones.

Headstream’s extensive global experience demonstrates how these panels perform reliably across different climates and operational scales, from compact laboratory suites to large-scale manufacturing halls.


Supporting Products for Comprehensive Facility Solutions

While Clean Room Panels serve as the primary envelope for controlled areas, Headstream offers complementary products that enhance complete project outcomes:

Insulated Panels(https://www.headstreampanel.com/products/insulated-panel/) deliver versatile thermal performance and structural strength for adjacent non-critical zones such as corridors, technical rooms, loading areas, or outer building shells. With options including polyurethane, rock wool, or glass wool cores, these general insulated panels help maintain design consistency while optimizing costs in less sensitive parts of the facility.

For areas requiring strong low-temperature control—such as chilled storage or processing sections—Cold Store Panels(https://www.headstreampanel.com/products/cold-store-panels/) provide specialized high-density insulation and cam-lock connection systems. They integrate effectively where clean environments transition into temperature-regulated storage, balancing cleanliness needs with thermal efficiency.

In supporting structures, staff facilities, or budget-conscious expansion areas, EPS Sandwich Panels(https://www.headstreampanel.com/products/eps-sandwich-panel/) offer a lightweight, economical solution with good thermal insulation and fast installation. Their clean appearance and reliable performance make them practical for warehouses, utility spaces, or secondary buildings surrounding the main clean production areas.

Sourcing from a single manufacturer ensures material compatibility, simplifies procurement, and streamlines coordination across the entire project.

Sustainability and Long-Term Operational Benefits

Modern clean room projects increasingly focus on energy efficiency and environmental responsibility. Headstream Clean Room Panels contribute through superior thermal insulation that reduces the energy demand of continuous HVAC operation—one of the highest cost factors in these facilities. Their modular design also minimizes construction waste and supports future modifications or relocations with less material impact.

Durable construction extends the service life of the clean room, reducing the need for frequent refurbishments and associated downtime. Lower maintenance requirements and consistent performance translate into higher operational uptime and more predictable costs over the facility’s lifespan.

Why Choose Headstream Clean Room Panels

Selecting the right panel system influences both initial construction success and decades of reliable operation. Headstream distinguishes itself through large-scale manufacturing capacity, strict quality assurance across multiple production bases, and dedicated technical support from design to after-sales service.

Key project benefits include:

  • Faster installation through modular assembly
  • Reduced energy consumption thanks to excellent insulation and airtightness
  • Simplified achievement of required environmental control standards
  • Flexible configurations that adapt to changing production needs
  • Reliable global supply chain with localized support

Whether you are planning a new high-tech manufacturing facility, upgrading an existing controlled environment, or expanding production capacity, Headstream Clean Room Panels offer a proven, high-performance foundation.

To review detailed specifications, discuss customization options, or explore how these panels can support your specific clean room project, please visit Headstream  official website(https://www.headstreampanel.com/).
Are PU Wall Panels Worth the Investment for Industrial Projects?

Introduction
In industrial construction, choosing the right building materials directly impacts long-term costs and performance. PU wall panels are gaining popularity, but are they truly worth the investment?

Cost vs Performance
PU panels may have a higher initial cost compared to traditional materials. However, their superior insulation significantly reduces energy consumption. Over time, this results in lower operational costs, especially for temperature-controlled environments.

Durability and Lifespan
PU panels are known for their long service life. With proper maintenance, they can last for decades without significant performance degradation. Their مقاومت to moisture and corrosion also reduces maintenance expenses.

Installation Efficiency
Another advantage is fast installation. Prefabricated panels can be installed quickly, reducing labor costs and project timelines.

Return on Investment (ROI)
When considering energy savings, reduced maintenance, and faster construction, PU panels offer strong ROI. Many industrial projects recover the initial investment within a few years.

Applications

  • Factories and production facilities
  • Warehouses and logistics centers
  • Cold storage buildings

Conclusion
PU wall panels are a cost-effective solution in the long run. Their energy efficiency, durability, and installation advantages make them a smart investment for industrial projects.

CTA
Want to improve your project’s efficiency and reduce costs? Contact HEADSTREAM for high-quality PU wall panel solutions.

Advantages and Application Scenarios of Handmade Rock Wool Cleanroom Panels

With the continuous improvement of industrial cleanliness and fire safety standards, handmade rock wool cleanroom panels are becoming increasingly popular in pharmaceutical factories, electronics workshops, hospitals, food processing plants, and other controlled environments. Compared with ordinary cleanroom panels, handmade rock wool cleanroom panels offer superior fire resistance, structural strength, and customization flexibility, making them an ideal solution for high-standard cleanroom projects.

What Are Handmade Rock Wool Cleanroom Panels?

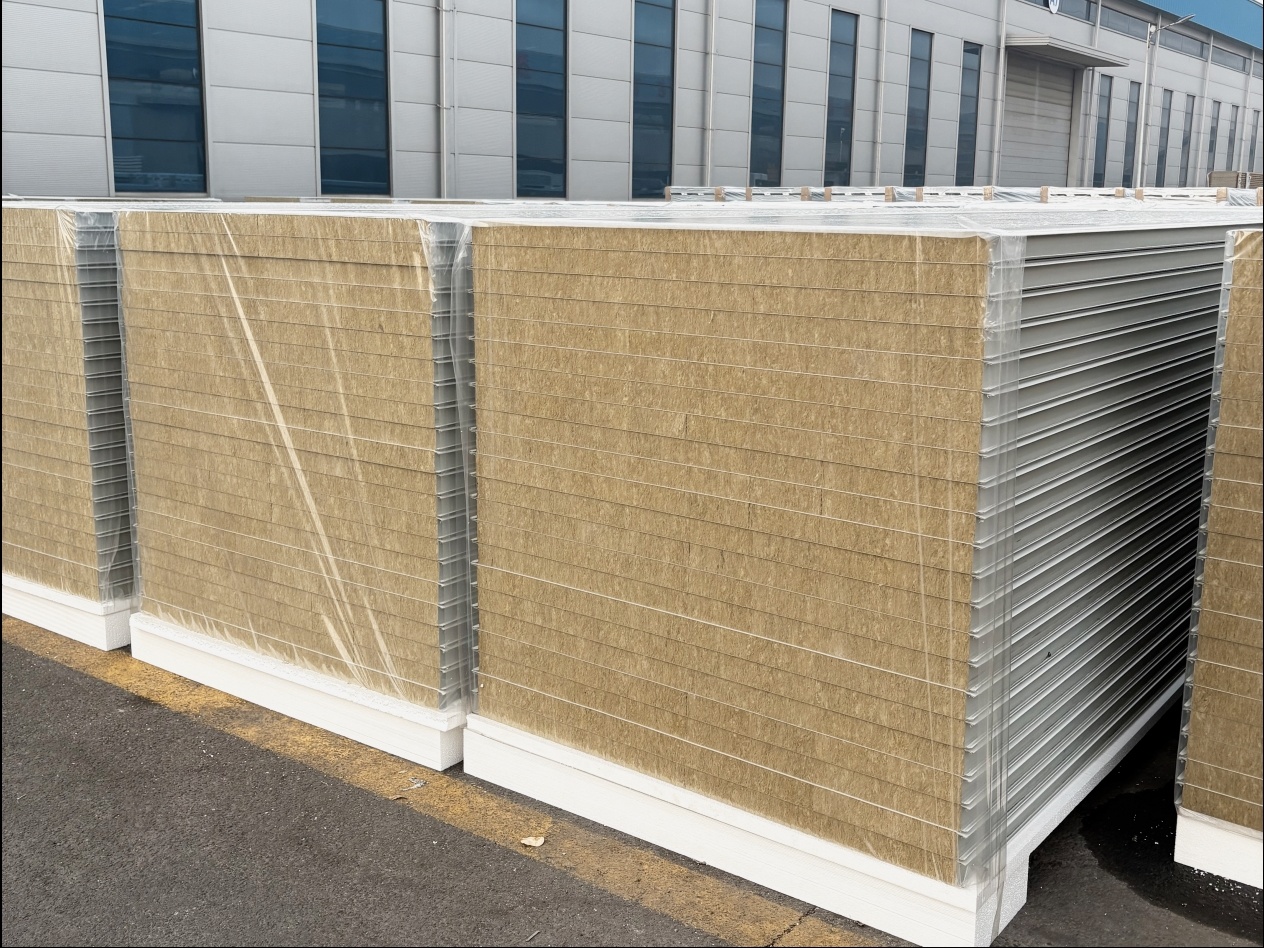
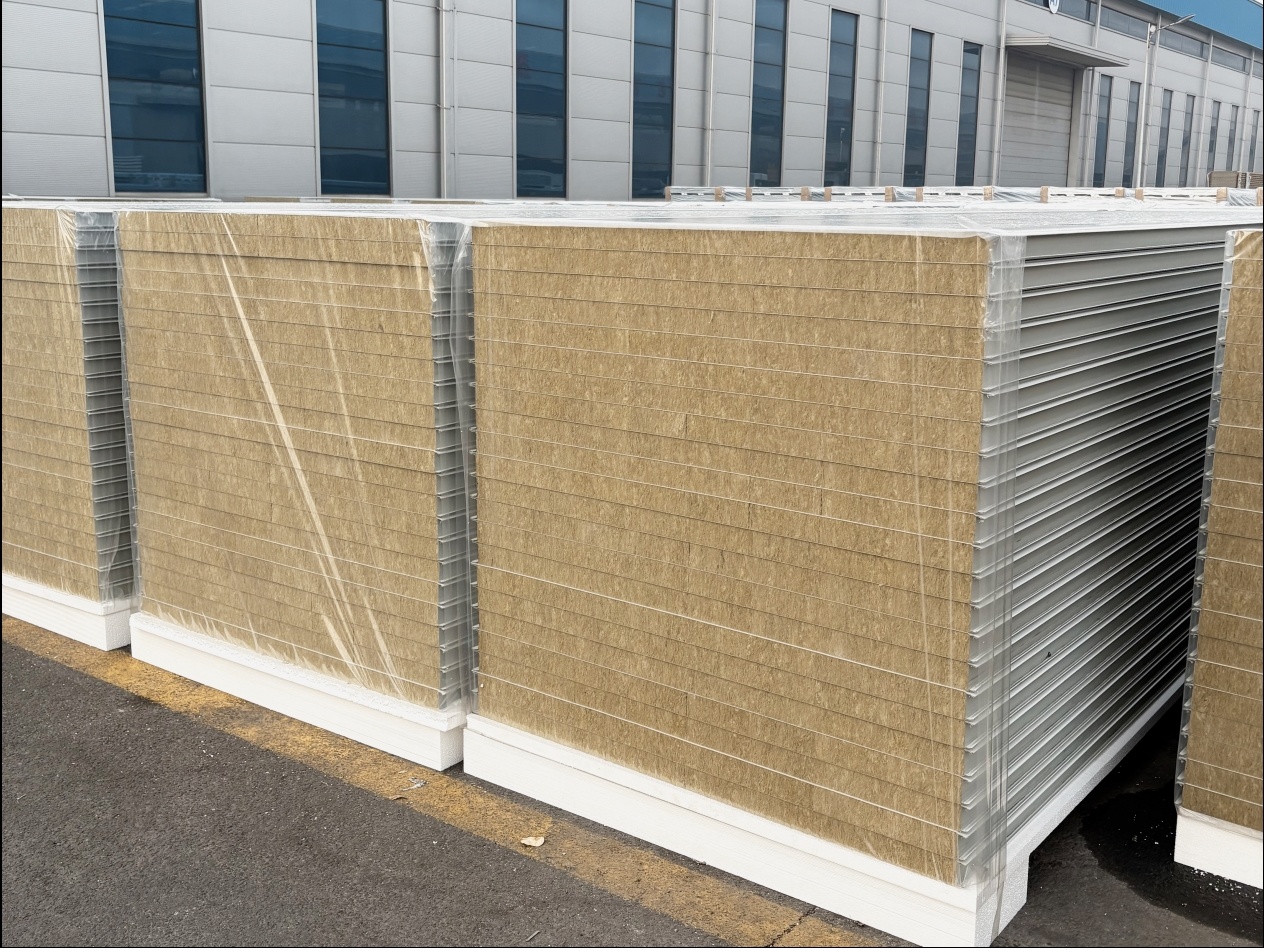
Handmade rock wool cleanroom panels are insulated sandwich panels manufactured through manual composite processes using high-density rock wool as the core material. The panel surfaces are typically made of color-coated steel sheets or stainless steel, combined with special edge sealing structures to improve airtightness and durability.

Unlike machine-made panels, handmade panels can be customized with different reinforcement structures and special functional requirements according to project demands.

Core Advantages of Handmade Rock Wool Cleanroom Panels

Excellent Fire Resistance

One of the biggest advantages of rock wool cleanroom panels is their outstanding fireproof performance. Rock wool is a non-combustible material with high melting temperature, which effectively helps prevent flame spread and improves overall building safety.

This makes handmade rock wool panels especially suitable for industries with strict fire protection requirements.

Superior Sound and Thermal Insulation

The dense fiber structure of rock wool provides excellent thermal insulation and sound absorption performance. These panels help maintain stable indoor temperatures while reducing equipment and environmental noise.

This improves both energy efficiency and working conditions in cleanroom facilities.

High Structural Strength

Handmade production processes allow additional reinforcement structures to be integrated inside the panels, improving load-bearing capacity and impact resistance.

As a result, handmade rock wool panels are more stable and durable in long-term industrial use.

Excellent Airtightness and Hygiene Performance

Cleanroom environments require strict control of dust and bacteria. Handmade cleanroom panels feature smooth surfaces and tightly sealed joints that help maintain high cleanliness standards and simplify daily cleaning and maintenance.

Flexible Customization

Compared with standard machine-made panels, handmade panels support more customized options, including:

  • Different panel thicknesses
  • Special reinforcement designs
  • Hidden joint systems
  • Custom dimensions
  • Fire-resistant upgrades

This flexibility allows them to meet complex cleanroom engineering requirements.

Typical Application Scenarios

Pharmaceutical Manufacturing

Pharmaceutical workshops require high levels of cleanliness, temperature control, and fire safety. Handmade rock wool cleanroom panels provide stable and safe partition systems for GMP-compliant facilities.

Food Processing Plants

Food factories need hygienic environments with easy-to-clean surfaces and moisture resistance. Rock wool cleanroom panels help maintain sanitary production conditions.

Electronics and Semiconductor Workshops

Precision electronics manufacturing requires dust-free environments and stable indoor temperatures. Handmade cleanroom panels support strict cleanroom standards while improving insulation performance.

Hospitals and Medical Facilities

Operating rooms, laboratories, and isolation wards require fire-resistant and antibacterial building materials. Handmade rock wool panels are widely used in modern healthcare construction.

Industrial Clean Workshops

Many industrial cleanrooms require both thermal insulation and fire resistance. Handmade rock wool panels provide reliable long-term performance in demanding industrial environments.

Why More Projects Choose Handmade Panels

As modern industrial buildings place greater emphasis on safety, energy efficiency, and customization, handmade rock wool cleanroom panels are increasingly replacing traditional partition materials.

Their combination of fireproof performance, structural strength, and cleanroom compatibility makes them an ideal solution for high-standard engineering projects worldwide.

Conclusion

Handmade rock wool cleanroom panels offer excellent fire resistance, insulation performance, structural stability, and customization flexibility for modern cleanroom construction. Widely used in pharmaceutical, food, medical, and electronics industries, they provide a safe, durable, and efficient solution for controlled environments requiring high cleanliness and fire safety standards.

PC Project

en_USEnglish
Free Quote & Information Request

Leave your inquiry, we will provide you with quality products and services!